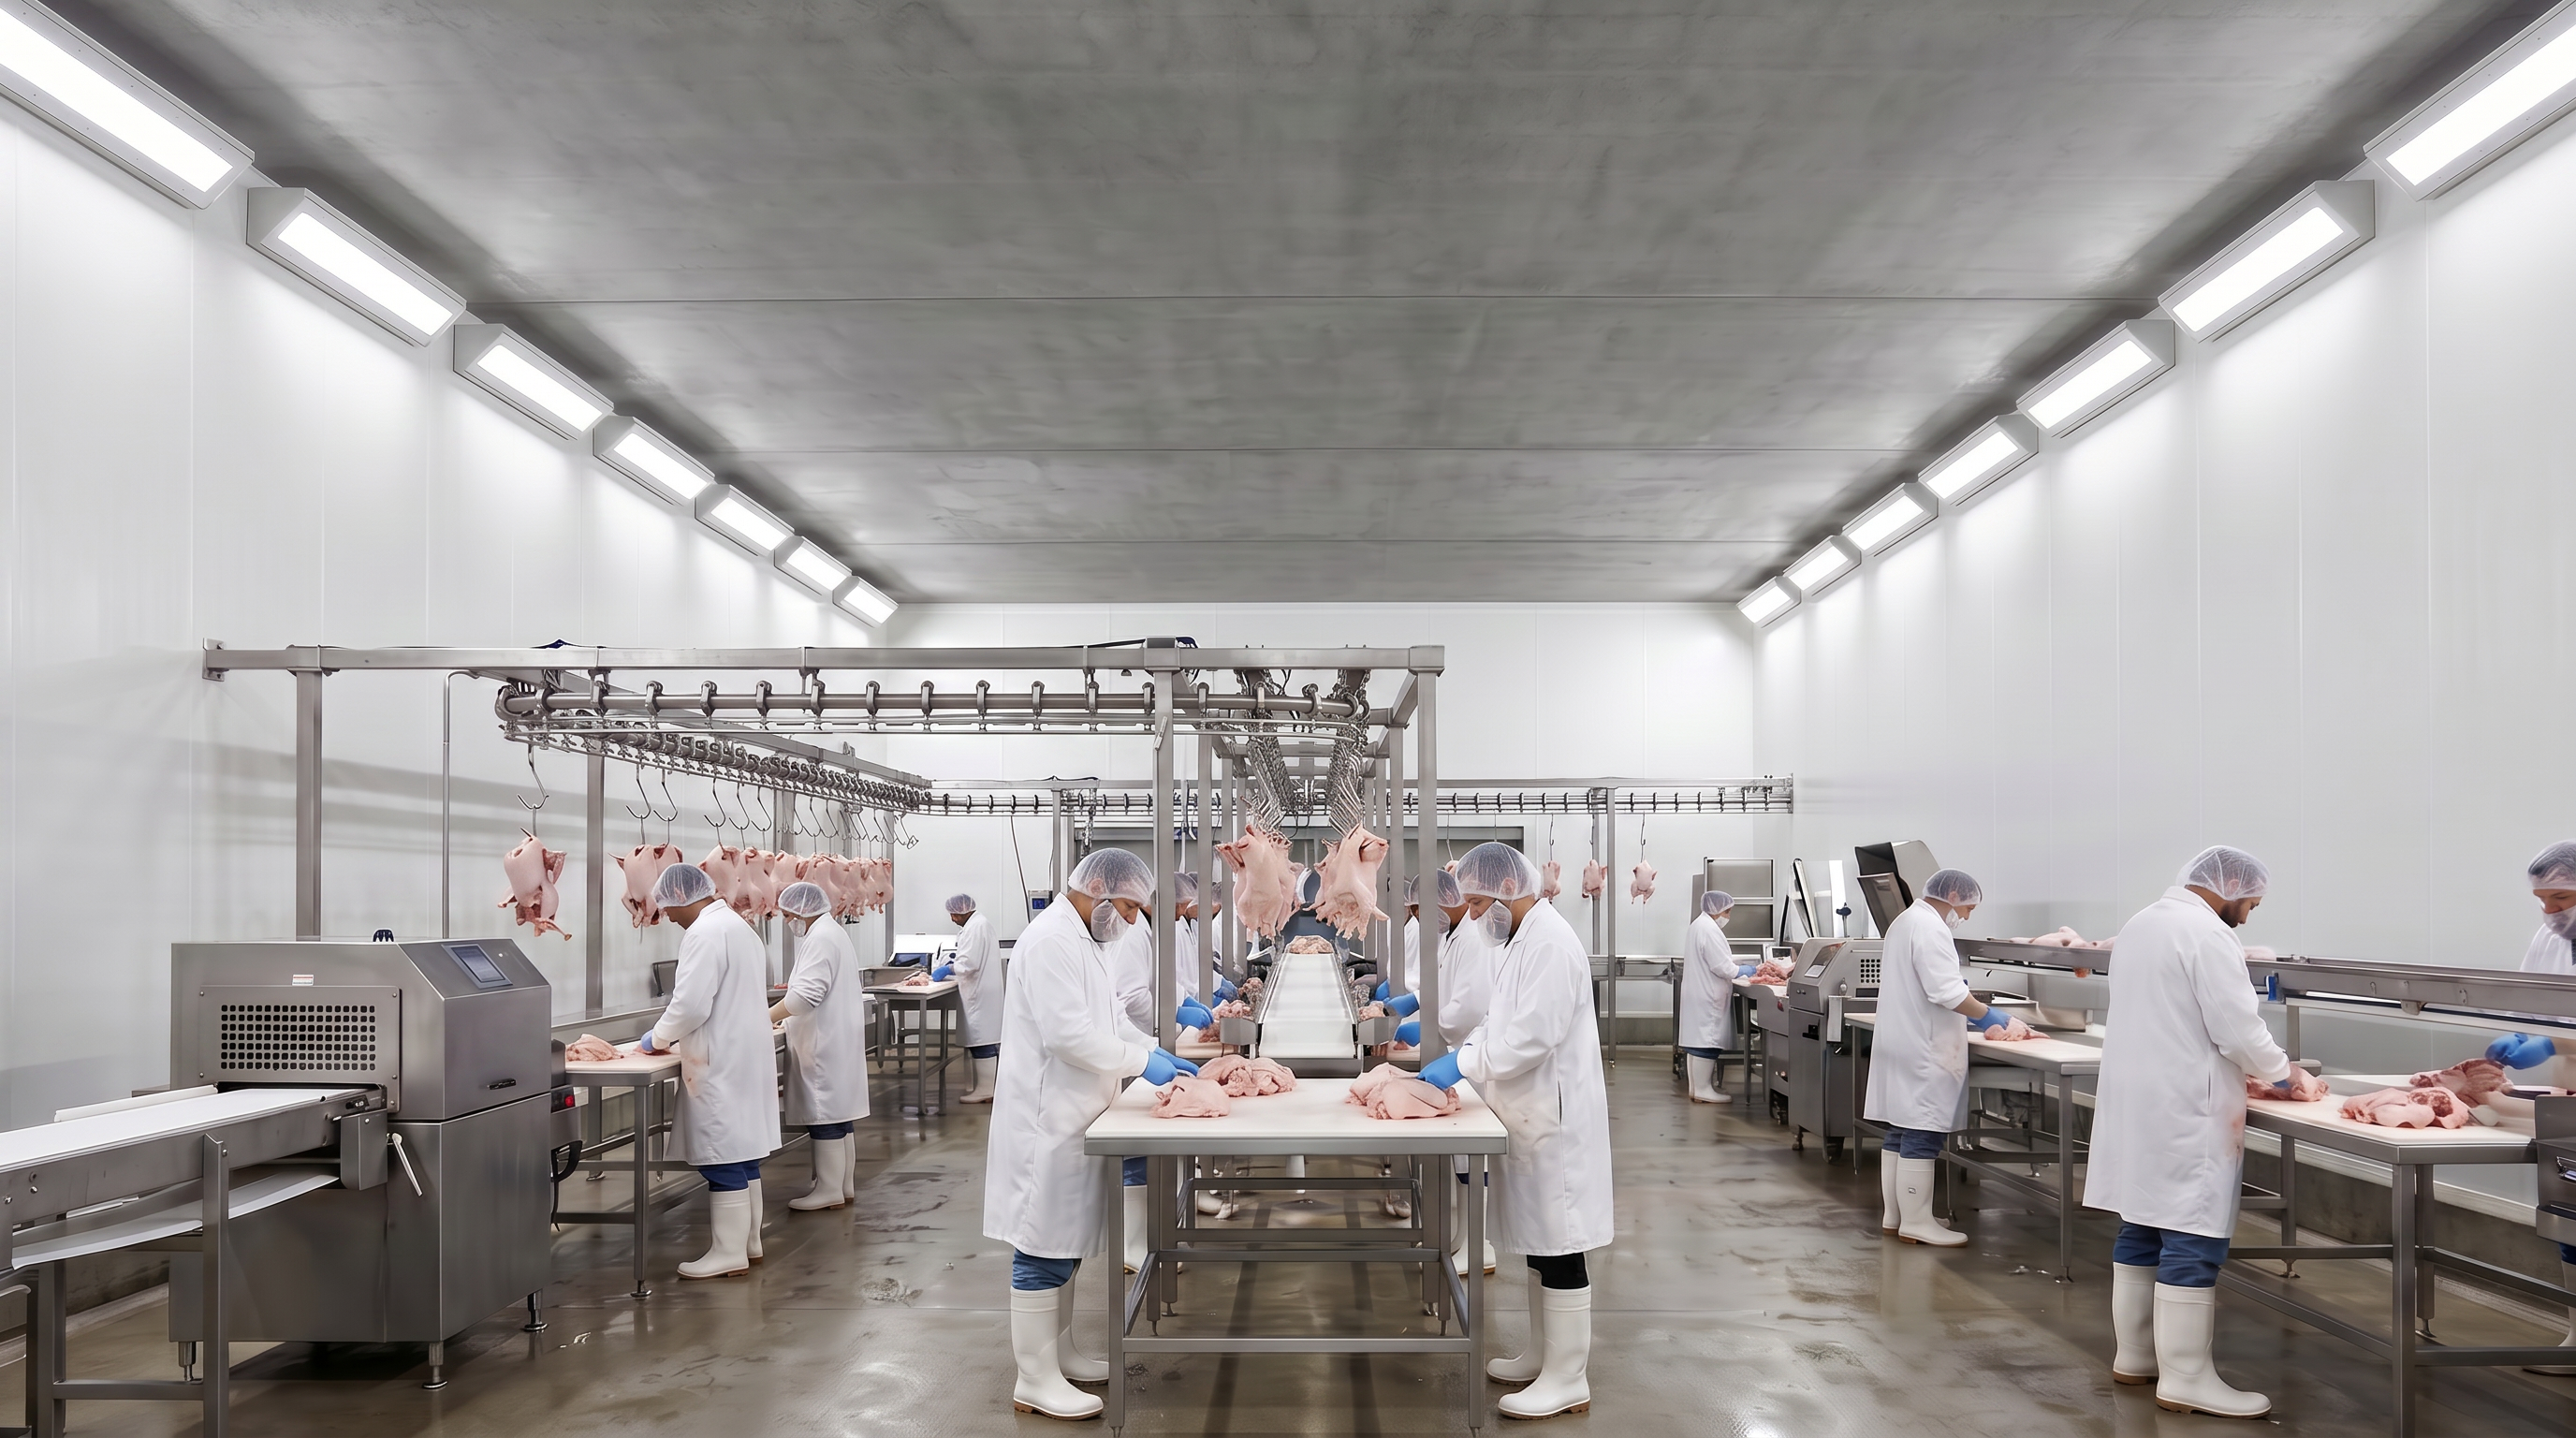
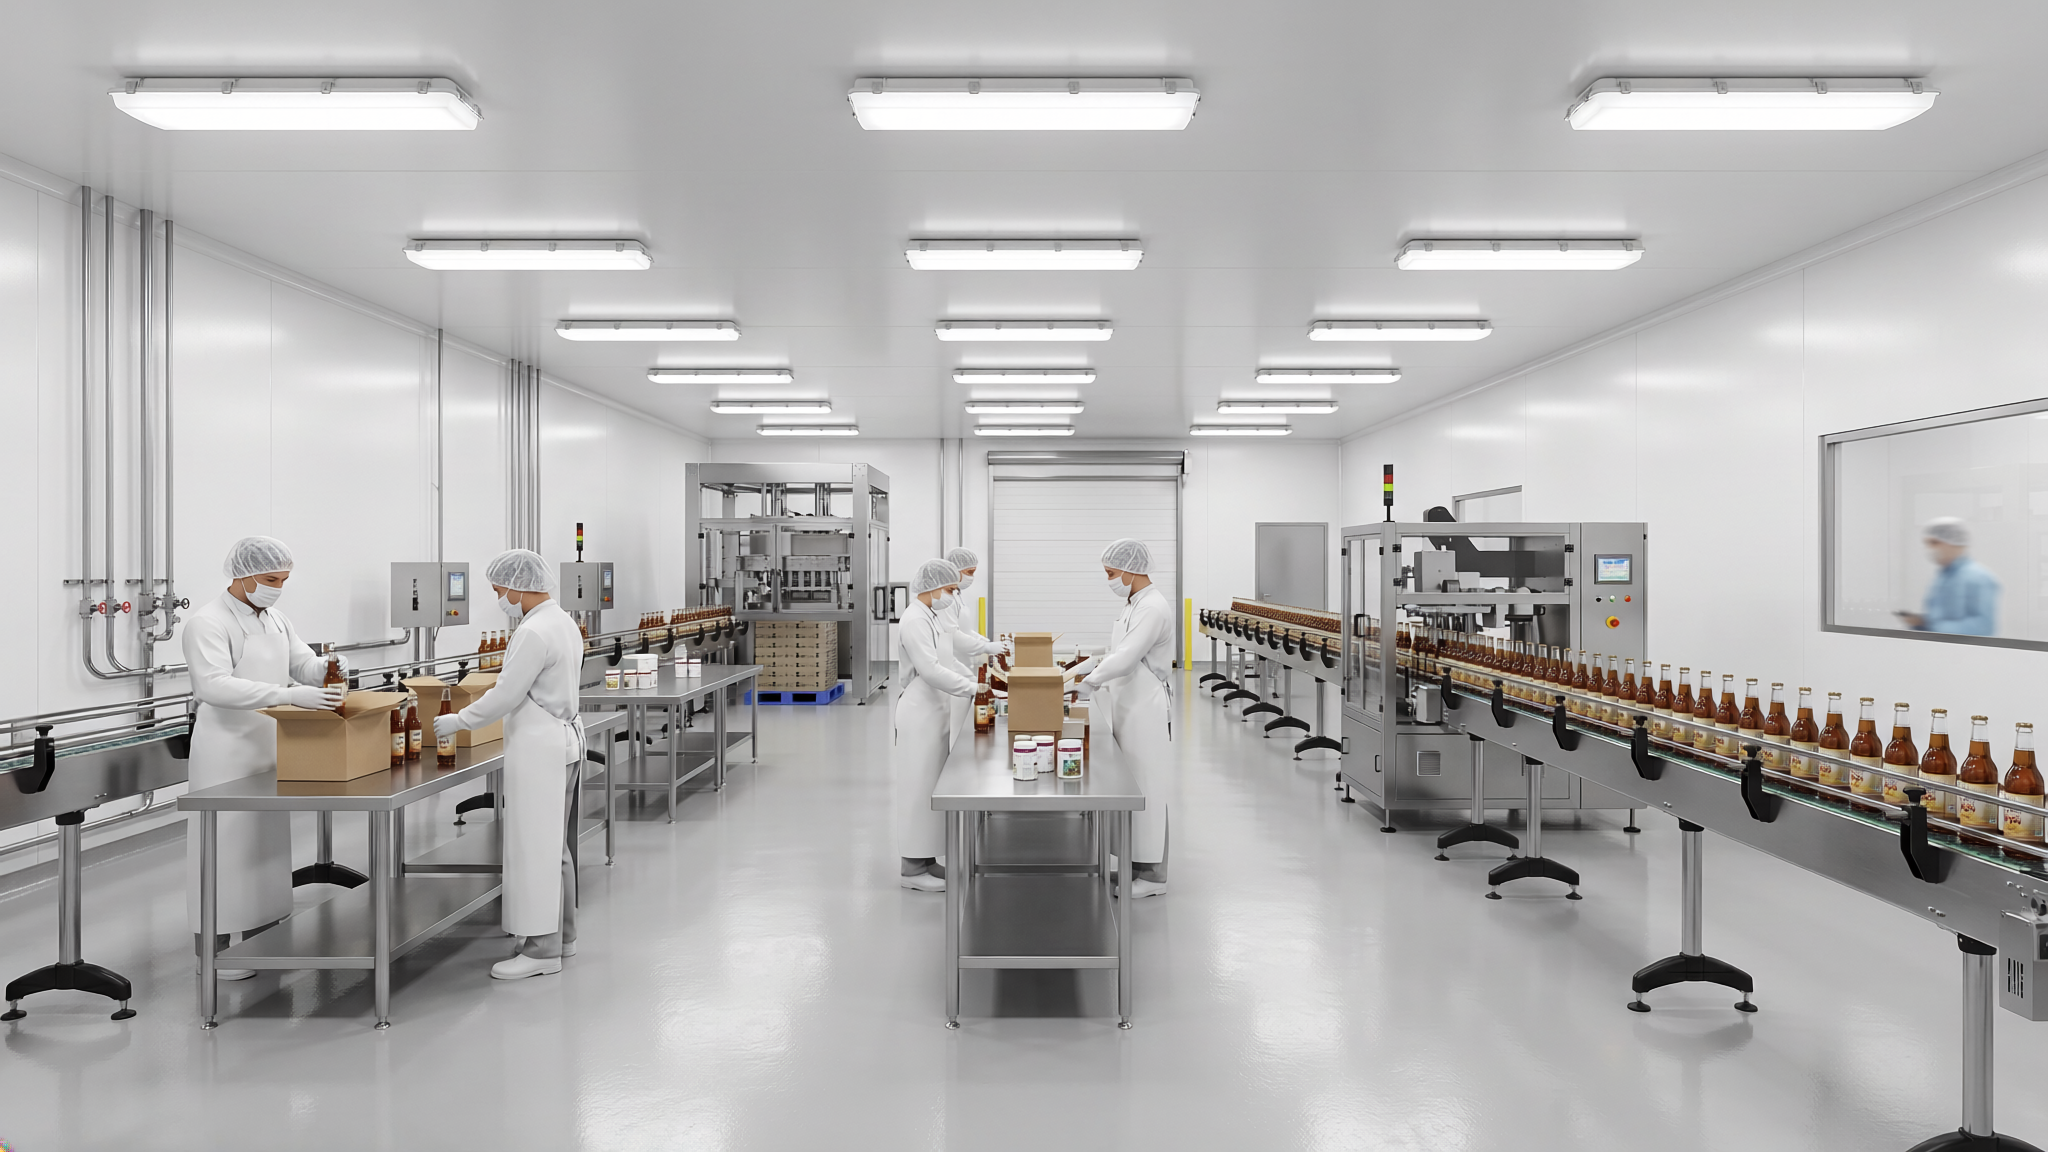
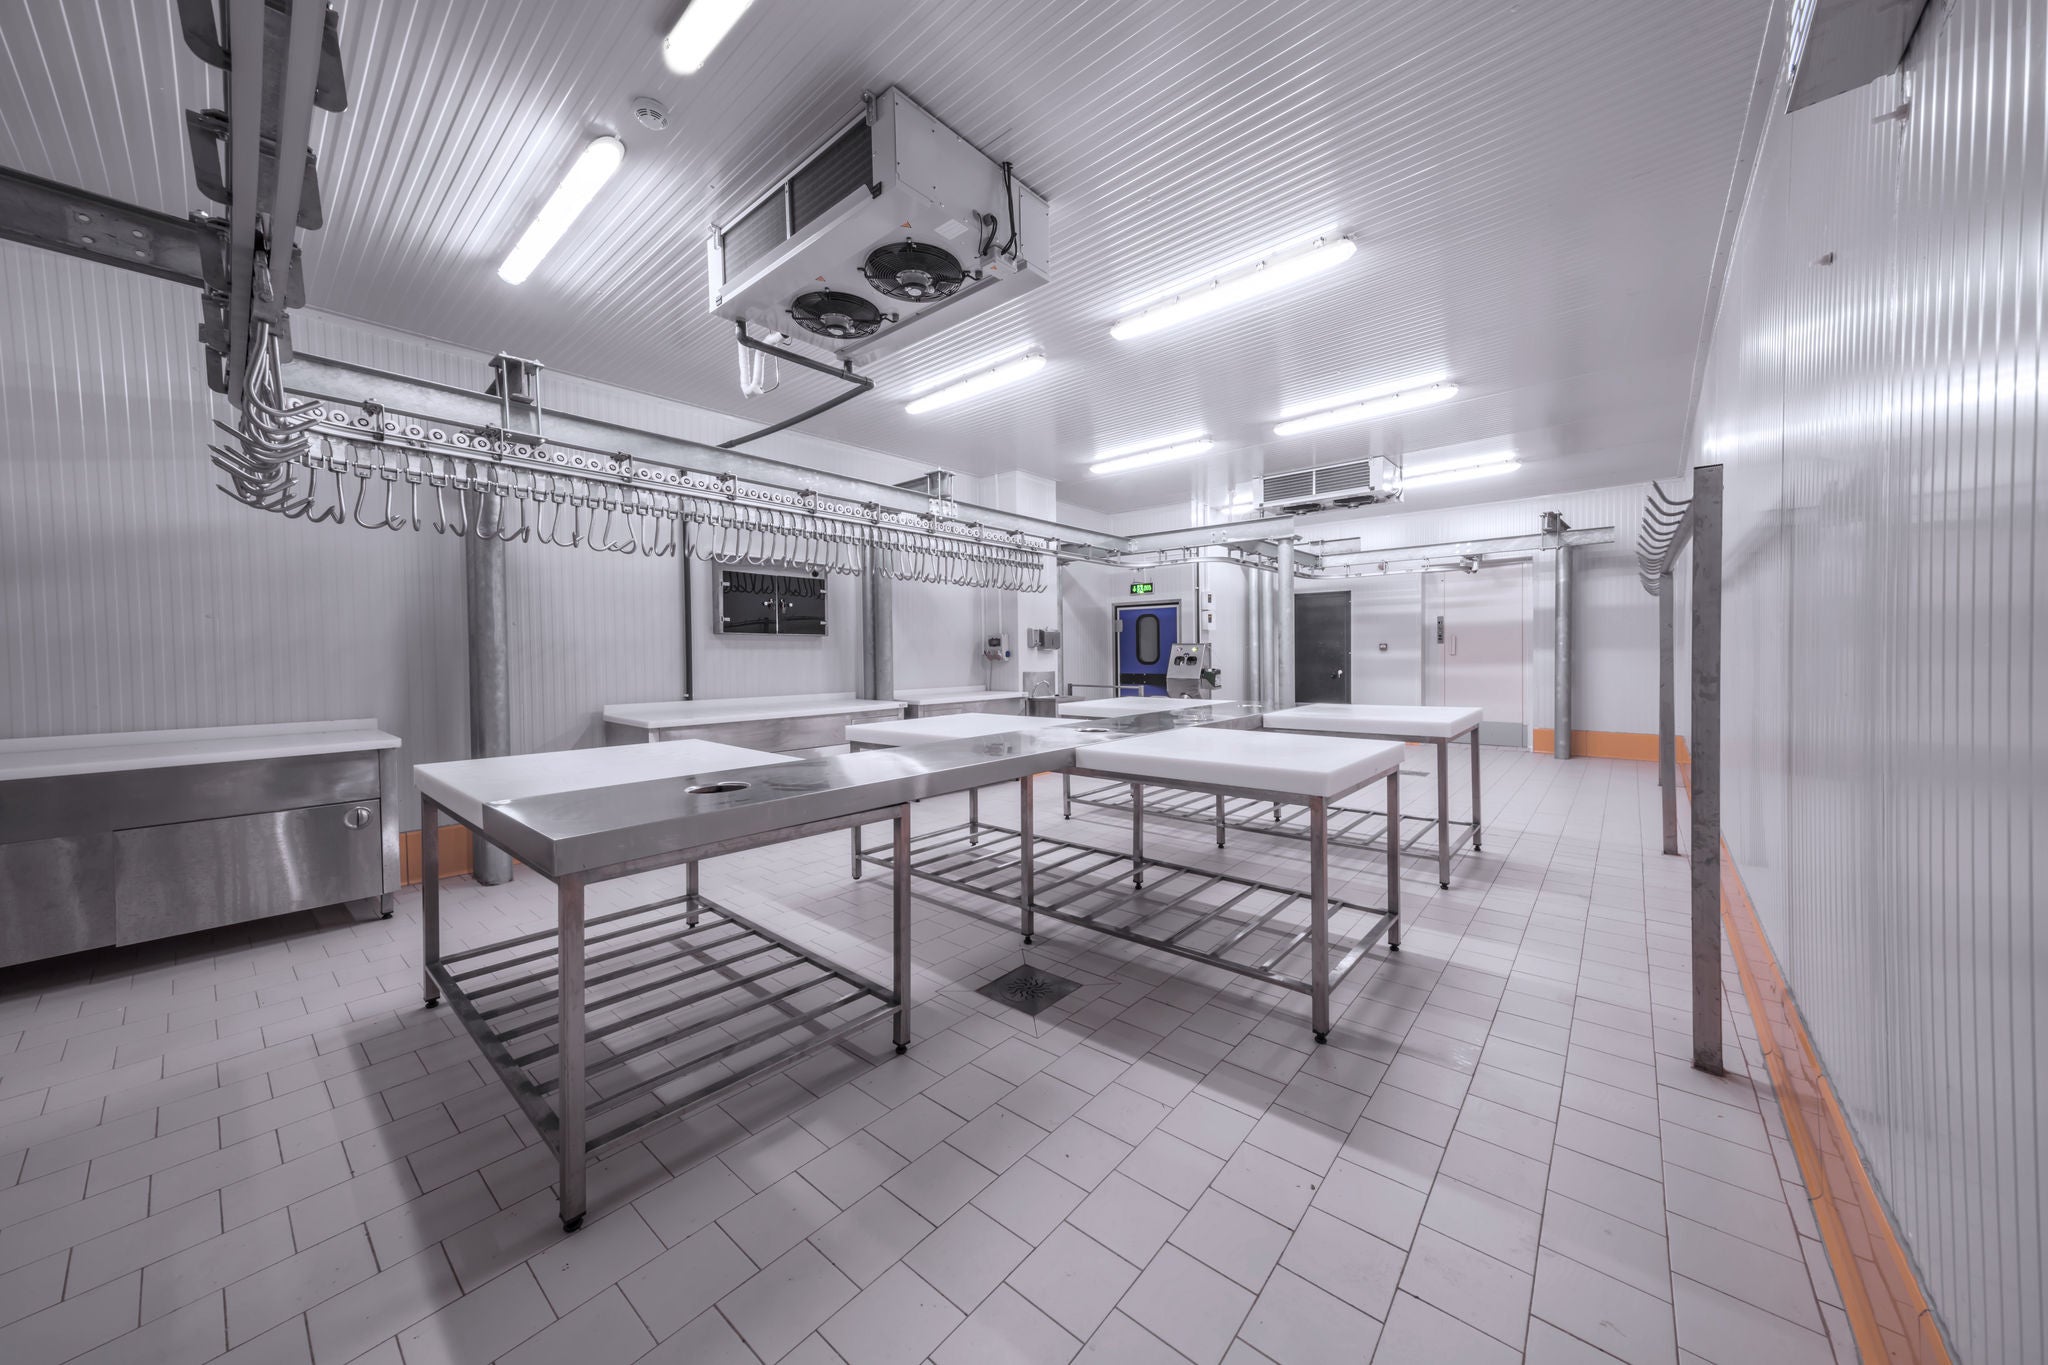
Every food processing facility faces the same challenge: maintaining strict sanitation standards while ensuring safe, productive operations. From raw ingredient handling and production lines to packaging areas, cold storage rooms, washdown zones, and support spaces, lighting must withstand harsh environments without compromising performance.
Certolux® Food Processing Lighting Solutions are engineered to help food manufacturers achieve exceptional cleanliness, visibility, operational efficiency, and long-term reliability. Designed for demanding food and beverage environments, our luminaires support sanitation requirements while delivering high-quality illumination that helps facilities operate with confidence.
Modern food processing environments require luminaires that resist moisture, corrosion, chemical exposure, and frequent washdowns while maintaining consistent performance. Industry-leading food processing lighting solutions commonly emphasize NSF certification, IP-rated protection, corrosion resistance, sealed construction, and washdown durability.